Table of Contents
- What Is a Machine Vision System in Aerospace & Defence Manufacturing?
- Why Is Component Inspection Critical in Aerospace & Defence?
- How Does a Machine Vision System Inspect Aerospace Components?
- What Defects Can a Vision System Machine Detect?
- How Does Machine Vision Improve Dimensional and Feature Verification?
- How Can Automated Vision Inspection Reduce Rework and Rejection?
- How Does a Machine Vision System Support Traceability and Quality Documentation?
- Which Aerospace & Defence Applications Can Use Machine Vision?
- What Should Manufacturers Consider When Choosing a Vision System?
- How Can QS Metrology Support Customized Vision Inspection?
- Frequently Asked Questions
In aerospace and defence manufacturing, a small visible defect or missing component feature can trigger additional inspection, production delays, or costly rework. Components must meet defined engineering specifications, and manufacturers need reliable methods to verify that critical visual and geometric characteristics remain consistent throughout production.
However, inspecting complex components manually can be challenging. Parts may contain multiple holes, slots, machined edges, connectors, markings, and assembly features. As production volumes increase and component designs become more intricate, relying exclusively on manual visual inspection can make consistent, repeatable quality checks difficult.
This is where a machine vision system can help.
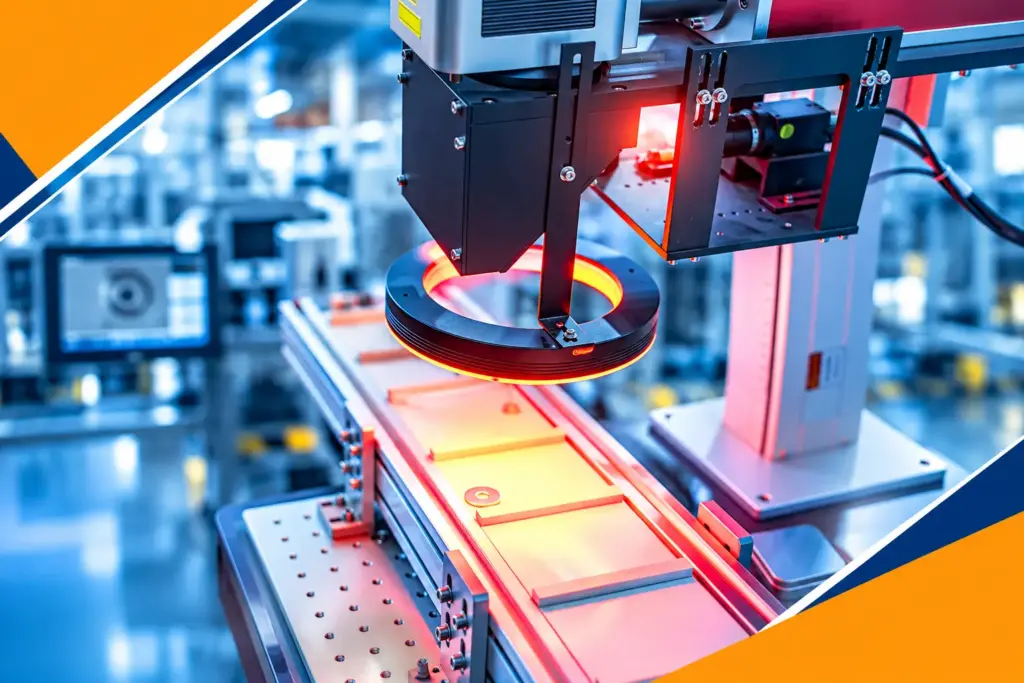
By combining industrial cameras, controlled lighting, optics, image-processing software, and automated decision-making, a machine vision system can inspect predefined component characteristics and compare them against established acceptance criteria. Depending on the application, the system can identify visible defects, verify feature presence, check component orientation, and communicate pass/fail results to production equipment.
For aerospace and defence manufacturers, this creates opportunities to strengthen visual quality control, standardize repetitive inspections, and identify non-conforming components before they proceed to subsequent manufacturing stages.
This article explains how a machine vision system can support aerospace and defence component inspection, which applications benefit from automated vision, and what manufacturers should consider when selecting a suitable solution.
What Is a Machine Vision System in Aerospace & Defence Manufacturing?
A machine vision system is an automated technology that uses cameras and software to capture, process, and evaluate images of components or products.
In aerospace and defence manufacturing, a customized vision system can help inspect visible characteristics such as component shape, hole presence, surface appearance, markings, part orientation, and assembly features.
A typical machine vision system may include:
- Industrial cameras for image acquisition.
- Lenses and optics for suitable image magnification and field of view.
- Controlled lighting to improve feature visibility.
- Image-processing software to analyze captured images.
- Sensors and triggers to synchronize inspection.
- Programmable logic controller (PLC) interfaces for communication with production equipment.
- Loading and sorting mechanisms where automated handling is required.
- Data logging and reporting features, depending on the system configuration.
The system compares captured images against predefined inspection rules or reference data. It can then generate an output such as PASS/OK or FAIL/NOT OK.
How Is a Vision System Machine Different from Manual Inspection?
Manual inspection relies on an operator examining the component and deciding whether its visible characteristics meet the applicable criteria.
A vision system machine performs configured image-analysis tasks using defined inspection parameters. This can improve consistency in repetitive inspection tasks and help manufacturers apply the same visual checks across multiple production cycles.
Inspection factor | Manual visual inspection | Machine vision inspection |
Inspection method | Human observation | Camera-based image analysis |
Repetitive checks | Can vary with operator and working conditions | Applies configured rules consistently |
Feature verification | Depends on visibility and inspection procedure | Can check predefined visible features |
Inspection speed | Depends on task and operator | Can support automated inspection at production speed |
Pass/fail decisions | Operator-based | Software-based against configured criteria |
Data recording | May require manual documentation | Can support automated data logging when configured |
Machine vision does not replace every inspection method. It is most effective when the required characteristics are visible, can be captured reliably, and can be evaluated using suitable imaging and analysis techniques.
Why Is Component Inspection Critical in Aerospace & Defence?
Aerospace and defence supply chains include a wide range of components, from machined brackets and housings to structural parts, electronic assemblies, connectors, and precision-fabricated components.
Each part has its own inspection requirements. Depending on the design, manufacturers may need to verify hole patterns, dimensions, markings, surface condition, component orientation, or the presence of specific features.
What Quality Problems Can Occur Without Consistent Inspection?
When inspection procedures are not sufficiently repeatable, manufacturers may face several challenges.
Missed visible defects: Scratches, dents, burrs, surface irregularities, and other visible defects may go unnoticed during inspection, depending on their size, contrast, and location.
Missing or incorrect features: A component may lack a required hole, slot, marking, fastener, connector, or other visible feature.
Part mix-ups: Similar-looking component variants may be confused during production, assembly, or packaging.
Inconsistent inspection decisions: Different operators may interpret borderline visual conditions differently unless acceptance criteria are clearly defined.
Late defect discovery: Problems detected only at a later production stage can require additional inspection, disassembly, rework, or rejection.
Documentation gaps: Manual inspection records may not capture every inspection result in a consistent and searchable format.
A suitably designed machine vision system can help address these challenges by standardizing selected visual checks and connecting inspection results with production workflows
Why Is Early Defect Detection Important in Aerospace Manufacturing?
When a defect is detected early, manufacturers have a better opportunity to isolate the affected part and investigate the process that produced it.
For example, if a machining operation begins producing components with a recurring visible burr or an incorrectly positioned feature, an automated vision inspection station may identify the issue before a larger quantity of parts progresses to assembly.
The system does not automatically establish the root cause. However, timely inspection results can help quality and production teams investigate the problem sooner.
How Does a Machine Vision System Inspect Aerospace Components?
A machine vision system works by capturing images under controlled conditions and evaluating them using configured inspection rules.
The exact design depends on the component, production environment, inspection criteria, and required throughput.
How Does the Camera Capture Component Images?
The inspection process begins when a component reaches the inspection position.
A sensor, trigger, or production-control signal can initiate image capture. Depending on the application, one camera or multiple cameras may be used to view different surfaces or features.
For example, a machined aerospace bracket may require inspection of its overall profile, mounting holes, and selected surface features. A single camera may be sufficient for some characteristics, while other applications may require several viewing angles.
Camera resolution, lens selection, working distance, image scale, and component positioning must be chosen according to the smallest feature or defect that needs to be evaluated.
Why Is Lighting Important in a Vision System?
Lighting determines how clearly a feature appears in the captured image.
Reflective metal surfaces, machined edges, curved housings, and recessed features can create challenging imaging conditions. Poor illumination may obscure a defect or create reflections that resemble one.
Depending on the inspection objective, the system may use:
- Backlighting to evaluate component silhouettes, openings, and profiles.
- Directional lighting to emphasize selected surface features.
- Diffuse lighting to reduce harsh reflections on suitable surfaces.
- Ring lighting to illuminate components from multiple directions.
- Multiple lighting arrangements to capture different characteristics of the same component.
The appropriate lighting method should be established through application testing using representative components and known defect samples.
How Does Vision Software Make a Pass/Fail Decision?
After capturing an image, the software processes the relevant region and evaluates the selected characteristics.
These may include dimensions, edges, shapes, feature presence, orientation, surface appearance, or visual patterns.
The results are compared with configured reference data, limits, or classification rules. If the system identifies a deviation outside the accepted criteria, it can generate a non-conformance result and send the output to connected production equipment
A typical workflow is:
Component positioning → Image capture → Image processing → Criteria evaluation → PASS/FAIL decision → Result recording or production action.
The effectiveness of this workflow depends on correct system design, suitable reference data, stable imaging conditions, and validation against the manufacturer’s inspection requirements.
What Defects Can a Vision System Machine Detect?
A vision system machine can be configured to identify different types of visible defects and non-conforming features. It is not limited to one universal defect library; its capabilities depend on the component and inspection application.
How Can a Vision System Identify Surface Defects?
When suitable optics and lighting make a defect visible, a machine vision system may detect:
- Scratches and surface marks.
- Dents and visible deformation.
- Burrs along selected edges.
- Surface discoloration.
- Visible contamination.
- Coating or finish irregularities.
- Certain cracks or surface discontinuities, where the imaging setup can reliably resolve them.
Defect detection must be validated against actual samples. Small, low-contrast, reflective, obscured, or subsurface defects may require other inspection techniques.
For aerospace and defence applications, machine vision should be treated as one part of the inspection strategy—not as a substitute for required non-destructive testing (NDT), material testing, or specialized crack-detection procedures.
How Can Machine Vision Detect Missing or Incorrect Features?
Feature-presence inspection is useful when components must contain specific holes, slots, openings, markings, or assembled elements.
For example, a vision system may be configured to check whether:
- Required holes are present.
- A slot has the expected visible shape.
- A connector or label is present.
- A component has the correct orientation.
- A selected feature is missing or visibly damaged.
- The part matches the expected variant.
The system compares the captured image with the configured inspection criteria and identifies deviations that it has been designed to detect.
Can a Vision System Inspect Different Component Variants?
Yes, a customized vision system can support multiple part types when the system includes suitable inspection recipes, reference data, and changeover procedures.
This can be useful for manufacturers producing different brackets, housings, panels, covers, and related components on the same production line.
Each variant should have its own verified inspection configuration. Part identification and recipe selection must also be controlled so that the system does not accidentally evaluate a component against the wrong reference.
How Does Machine Vision Improve Dimensional and Feature Verification?
Aerospace and defence components may include multiple geometric features that need to be checked against engineering drawings or predefined tolerances.
A properly configured vision system can measure selected two-dimensional features from captured images. Depending on the optics, calibration, camera arrangement, and software, these checks may include lengths, diameters, distances, angles, profiles, and hole positions in the image plane.
Which Dimensions Can a Machine Vision System Check?
Potential inspection parameters include:
- Overall visible length and width.
- Hole diameter and spacing.
- Distance between selected edges.
- Slot width and length.
- Visible profile and contour.
- Angles between defined edges.
- Relative position of selected features.
- Presence and location of designated markings.
These measurements are useful only when the optical setup and measurement method are suitable for the required tolerance.
For high-precision aerospace applications, the system must be evaluated for measurement uncertainty, repeatability, calibration, environmental stability, and traceability to appropriate measurement standards.
Can a Vision System Replace a Coordinate Measuring Machine?
Not in every application.
A machine vision system is well suited to automated inspection of visible features and selected dimensions. A coordinate measuring machine (CMM) may be more appropriate when a component requires detailed three-dimensional measurements, geometric dimensioning and tolerancing (GD&T) evaluation, or access to features that cannot be measured reliably through the selected camera arrangement.
Some manufacturers may use both technologies: machine vision for fast in-line checks and a CMM or another suitable metrology method for more comprehensive dimensional verification.
The correct choice depends on the drawing requirements, tolerances, component geometry, inspection frequency, and required measurement confidence.
How Can Automated Vision Inspection Reduce Rework and Rejection?
Rework and rejection costs can increase when a defect remains undetected until the component has passed through several manufacturing stages.
Automated vision inspection can help identify selected non-conformities closer to the process where they occur.
How Does a Machine Vision System Help Prevent Defective Parts from Moving Forward?
When a component fails the configured inspection criteria, the system can communicate the result to a PLC, robot, conveyor, or sorting mechanism.
Depending on the design, the production process may:
- Divert the component to a rejection bin.
- Route the component to a manual inspection station.
- Stop or pause the process for investigation.
- Record the failure for quality review.
- Alert an operator to a recurring defect pattern.
These actions can help prevent known non-conforming parts from being mixed with accepted components.
The specific action should be designed according to the risk associated with the part, the production process, and the manufacturer’s quality procedures.
How Can Automated Inspection Improve Production Efficiency?
Manual inspection can become a bottleneck when a production line generates more parts than operators can inspect within the required cycle time.
An appropriately engineered vision system can perform defined checks automatically while parts move through the inspection station or are presented to it.
Potential operational benefits include:
- More consistent repetitive inspections.
- Faster identification of selected visible defects.
- Reduced dependence on manual visual screening for suitable tasks.
- Less unnecessary handling of inspected components.
- Improved separation of accepted and rejected parts.
- Better information for process-improvement activities.
Actual throughput and cost savings depend on the inspection complexity, line speed, part handling, system availability, false-reject rate, and integration requirements.
How Does a Machine Vision System Support Traceability and Quality Documentation?
Aerospace and defence manufacturers often need to maintain controlled inspection records and demonstrate that their quality procedures have been followed.
A machine vision system can support documentation when data capture and storage features are included in its design.
What Inspection Data Can a Vision System Record?
Depending on the configuration, a system may record:
- Part or component identifier.
- Batch or production reference.
- Inspection date and time.
- PASS/FAIL result.
- Measured values for configured parameters.
- Captured inspection images.
- Defect classifications.
- Rejection counts and inspection statistics.
- Operator or station details.
This information can help quality teams investigate recurring defects, compare production batches, and review the performance of inspection processes.
How Can a Vision System Improve Traceability?
Where the application requires part-level tracking, the system may be integrated with barcode readers, QR-code readers, production databases, or manufacturing execution systems.
Inspection results can then be associated with the relevant component, batch, or production event.
However, traceability is not automatic simply because a camera is installed. Identification, data storage, retention, access control, and system integration must be designed to meet the manufacturer’s documented requirements.
For aerospace and defence programmes, any additional requirements concerning data security, records retention, or controlled production information should be addressed separately in the system specification.
Which Aerospace & Defence Applications Can Use Machine Vision?
Machine vision is most useful when an inspection requirement can be expressed as a set of observable features, measurable characteristics, or visual acceptance criteria.
How Can Machine Vision Inspect Machined Aerospace Components?
Machined brackets, housings, mounting plates, covers, and other precision components may require checks for hole presence, slot geometry, component outline, visible burrs, and selected dimensions.
A camera-based inspection station can evaluate these characteristics against approved reference data before the component moves to the next manufacturing stage.
For more complex geometric requirements, machine vision may be combined with CMM inspection or other dimensional metrology techniques.
How Can a Vision System Support Defence Equipment Assembly?
Defence equipment can include panels, housings, control assemblies, connectors, brackets, and other components with defined assembly features.
A vision system may be configured to check the presence, orientation, position, or visible condition of selected components before the assembly is released to the next stage.
Examples include confirming that a required connector is present, a visible label matches the selected configuration, or specified mounting features are correctly positioned.
The system should be designed around the approved assembly specification and validated using representative conforming and non-conforming samples.
How Can Machine Vision Inspect Electrical and Electronic Assemblies?
Electrical and electronic assemblies may contain connectors, terminals, labels, fasteners, and other visible features that need to be present and correctly positioned.
Machine vision can support selected presence/absence checks, orientation verification, marking inspection, and visible assembly inspection.
It should not be assumed to detect internal electrical failures, hidden solder defects, or other faults that are not observable in the captured images. Such requirements may need electrical testing, X-ray inspection, or other appropriate techniques.
How Can Machine Vision Support Final Inspection Before Dispatch?
At the final inspection stage, a customized vision system may verify selected external characteristics, component identity, visible damage, labels, and other defined requirements.
This can provide an additional automated checkpoint before packaging or dispatch.
Final acceptance should still follow the applicable inspection plan and customer requirements. A visual inspection result alone does not certify every dimensional, material, structural, or functional characteristic of an aerospace or defence component.
What Should Manufacturers Consider When Choosing a Vision System?
Selecting a machine vision system starts with the inspection problem—not with the camera alone.
Manufacturers should define the characteristics that must be checked, the smallest relevant defect, the required tolerance, the production rate, and the action needed when a component fails inspection.
Which Technical Factors Matter Most?
- Inspection objective
Specify whether the application requires defect detection, dimension measurement, feature-presence checks, part identification, orientation verification, or a combination of tasks.
- Camera resolution and optics
The camera and lens must capture the required features at an image scale suitable for the inspection tolerance.
- Lighting design
Reflective, dark, curved, and textured surfaces may require different illumination arrangements. Test the lighting on representative samples.
- Component positioning
Repeatable positioning helps the system capture consistent images. The application may need fixtures, guides, sensors, or automated handling.
- Inspection speed
The system must complete image capture and processing within the available production cycle time.
- Software and algorithms
Choose image-processing or AI-based methods according to the inspection problem. Any model or algorithm should be validated using representative good parts, known defects, and expected production variation.
- Automation and integration
Determine whether the system must communicate with a PLC, conveyor, robot, reject mechanism, or existing quality software.
- Data and reporting
Specify what information must be stored, how results are identified, and how inspection records will be accessed.
- Measurement confidence and validation
Where dimensional measurement is required, define calibration, repeatability, measurement uncertainty, and acceptance criteria before deployment.
- Service and application support
Consider system commissioning, operator training, maintenance, technical support, and the ability to adapt inspection recipes when component designs change.
How Should Manufacturers Validate a Machine Vision System Before Production?
A practical validation process should include:
- Define the inspection characteristics and acceptance limits.
- Collect representative conforming and non-conforming components.
- Test camera, optics, and lighting configurations.
- Establish the inspection algorithm and reference data.
- Evaluate detection performance, including false accepts and false rejects.
- Test repeatability across expected operating conditions.
- Confirm cycle time and integration with production equipment.
- Document the validated inspection procedure.
- Train operators and establish a response process for failed or uncertain results.
This helps ensure that the selected system addresses the real inspection requirement rather than simply producing clear-looking images.
How Can QS Metrology Support Customized Vision Inspection?
QS Metrology provides machine vision and in-line inspection solutions designed around manufacturing inspection and automation requirements.
Its published machine vision capabilities include industrial cameras, optics, controlled lighting, image-processing software, customized inspection logic, multiple-camera arrangements, and integration with production equipment and sorting mechanisms.
The company also describes applications involving feature-presence checks, shape inspection, component sorting, and production-result logging.
What Can a Customized Vision System Include?
Depending on the application, a solution may include:
- Camera and lens selection.
- Lighting and imaging design.
- Image-processing software.
- Configurable inspection parameters.
- Multiple-camera arrangements.
- Sensors and triggers.
- PLC and production-equipment interfaces.
- Automated loading and sorting.
- PASS/FAIL decision logic.
- Inspection statistics and data logging.
For aerospace and defence manufacturers, the starting point should be a clearly defined inspection requirement, supported by representative samples and the applicable engineering specifications.
QS Metrology can assess the application requirements and help determine whether a customized vision system is suitable or whether another metrology or inspection method is needed for particular characteristics.
Explore the QS Metrology In-Line Inspection Systems to learn more about its machine vision capabilities.
How Can a Machine Vision System Improve Aerospace & Defence Quality Control?
Aerospace and defence manufacturers must maintain consistent inspection procedures for components with demanding quality requirements. Manual visual inspection remains useful for many tasks, but repetitive checks at higher production volumes can benefit from automation.
A properly designed machine vision system can inspect selected visible defects, verify feature presence, check component orientation, measure suitable two-dimensional characteristics, and communicate pass/fail results to production equipment.
When integrated into a controlled inspection workflow, a vision system can help manufacturers identify certain defects earlier, improve the consistency of repetitive checks, and create more useful inspection records.
The key is selecting a solution that matches the component geometry, required tolerances, production environment, and documented acceptance criteria. Machine vision should complement other inspection and metrology methods wherever the required characteristics cannot be verified reliably through imaging alone.
Planning to automate component inspection in your aerospace or defence manufacturing process? Discuss your inspection requirements with QS Metrology to evaluate a customized vision solution for your application.
Discuss Your Aerospace Component Inspection Requirements
Frequently Asked Questions
What is a machine vision system used for in aerospace manufacturing?
A machine vision system is used to automate selected visual inspections, including surface-defect detection, feature-presence checks, component identification, orientation verification, and suitable dimensional measurements. Its capabilities depend on the camera, optics, lighting, software, and inspection criteria.
How does a vision system machine detect defects in aerospace components?
A vision system machine captures images under controlled lighting and analyzes them using predefined image-processing rules or suitable AI-based algorithms. It compares the observed characteristics against reference data or acceptance criteria and generates a result. Detection performance must be validated using representative components and defects.
Can a machine vision system measure aerospace component dimensions?
Yes, a suitably configured machine vision system can measure selected two-dimensional characteristics, such as hole diameters, distances, angles, and visible profiles. Accuracy depends on calibration, optics, image scale, component positioning, and the required tolerance. Complex three-dimensional measurements may require a CMM or another suitable metrology method.
Can machine vision replace manual inspection and non-destructive testing?
Machine vision can automate appropriate repetitive visual checks, reducing reliance on manual inspection for those tasks. It does not replace all manual inspection or specialized non-destructive testing. Hidden defects, internal flaws, material properties, and other non-visible characteristics may require different inspection methods.
How do manufacturers choose the right vision system for aerospace and defence components?
Manufacturers should define the inspection objective, required defect sensitivity, dimensional tolerances, component geometry, production speed, lighting conditions, data requirements, and automation interfaces. Testing representative good and defective samples before deployment helps validate whether the proposed vision system meets the inspection requirements.